Finishing sintered tungsten carbide is different from shaping material before sintering. Once cemented carbide has its final hard structure, the features and tolerances usually need a process chosen specifically for that material.
Review the carbide machining and finishing options against the complete drawing.
Separate the material stages
| Stage | What changes the process discussion |
|---|---|
| Before final sintering | Intermediate material can be shaped with shrinkage and final requirements in mind |
| Sintered blank | Hardness and brittle behavior affect material removal and edge handling |
| Finished component | Geometry, surface integrity and inspection define acceptance |
Do not assume a conventional steel-machining route transfers directly to sintered carbide. Thin features, unsupported edges and abrupt transitions need particular care. Diamond grinding and electrical discharge machining can address different geometry needs; the complete drawing determines which route is practical.
Explain the feature, not just the machine name
For an outside diameter, provide length, support geometry and required finish. For a slot or internal profile, show access, corner limits and any surfaces that need subsequent finishing. A selected process must leave an acceptable component, not merely remove the right volume of material.
Extramet’s service pages describe its offered capabilities. Ask the quote to confirm the owner of each proposed operation, including any subcontracted step. The discussion here is about process selection and does not claim that every carbide manufacturing method is performed in-house.
Carbide is hard for a reason
Tungsten carbide is a composite material made from hard carbide particles bonded with a metallic binder, commonly cobalt or nickel depending on the grade and application. The carbide phase provides wear resistance. The binder helps with toughness and manufacturability. Changing grain size and binder content changes how the material behaves in service and during finishing.
This is why carbide is not just “hard steel.” It is a different material system. Cutting tools that work on steel may wear rapidly or fail when applied to carbide, especially after sintering.
Grinding is often the practical route
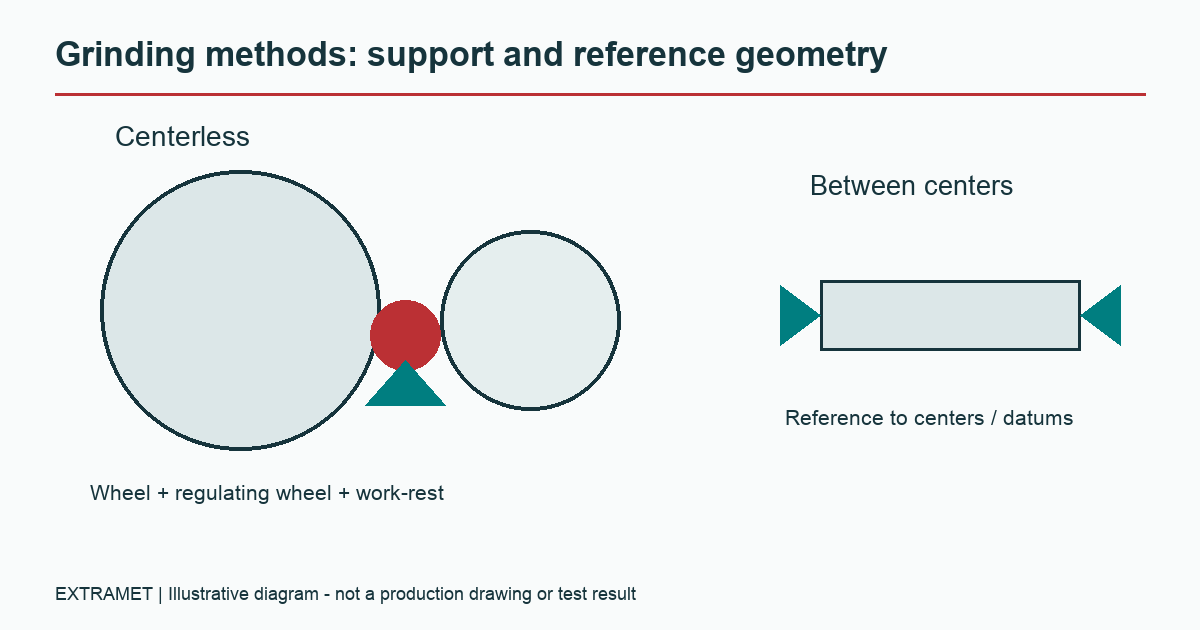
Many carbide parts are formed close to size and then finished by grinding. OD grinding, centerless grinding, surface grinding, and related finishing methods can bring parts into tolerance while controlling surface condition. For round parts, centerless grinding or CNC cylindrical grinding may be used depending on geometry and print requirements.
Grinding is not just a finishing step. It can determine whether the part fits, seals, tracks, or wears correctly. Surface finish, roundness, straightness, and edge condition all affect performance.
EDM and lapping may be needed
When a carbide part has holes, slots, fine features, or complex geometry, EDM may be part of the manufacturing path. Lapping or polishing may be needed when flatness, finish, or sealing behavior is critical. The right combination depends on the grade, geometry, and tolerance requirements.
Trying to force every carbide part through one process can increase cost or risk. A better approach is to match the process to the feature that actually controls performance.
Design choices affect machining cost
Small radii, deep features, extreme tolerances, long slender sections, and unnecessary finish requirements can all add cost. This does not mean buyers should loosen functional requirements. It means every requirement should have a reason. If a tolerance is critical, keep it. If it is inherited from a legacy print and not functional, review it before quoting.
Carbide’s material capabilities are strongest when grade, geometry, and finishing method are planned together.
What to send for review
Send the drawing, grade or performance need, tolerance requirements, quantity, and application notes. If the part is replacing steel, include the failure mode. If the part is part of a larger assembly, describe fit and wear conditions. The more context Extramet has, the easier it is to recommend a manufacturable path.
Start with the Request for Quote form when you are ready for a production review.
Compare EDM and diamond grinding when feature access and final surface integrity determine the process.
Use the surface-finish callout guide to state the parameter, units, marked surface and measurement basis.
Product questions? Contact Michael Douglas, Extramet Products product expert and Sales and Marketing contact.